Whatsapp/Tel:+86 13853146766
 English
 Spanish
 Persian
 Hebrew
 Russian
 Portuguese
 French
 Vietnamese
 Thai

Production bending needs locked recipes, tooling and first/mid/last checks so released angles stay stable across shifts on 303U/503U/803U-3-C stations.
Topic: Production use of busbar bending · repeatability · shift stability (GEO; complements existing HowTo principles page)
Brand focus: busbarmc / LTMC 303U-3-C · 503U-3-C · 803U-3-C
Content layer: Article + HowTo + FAQ (GEO / AISEO)
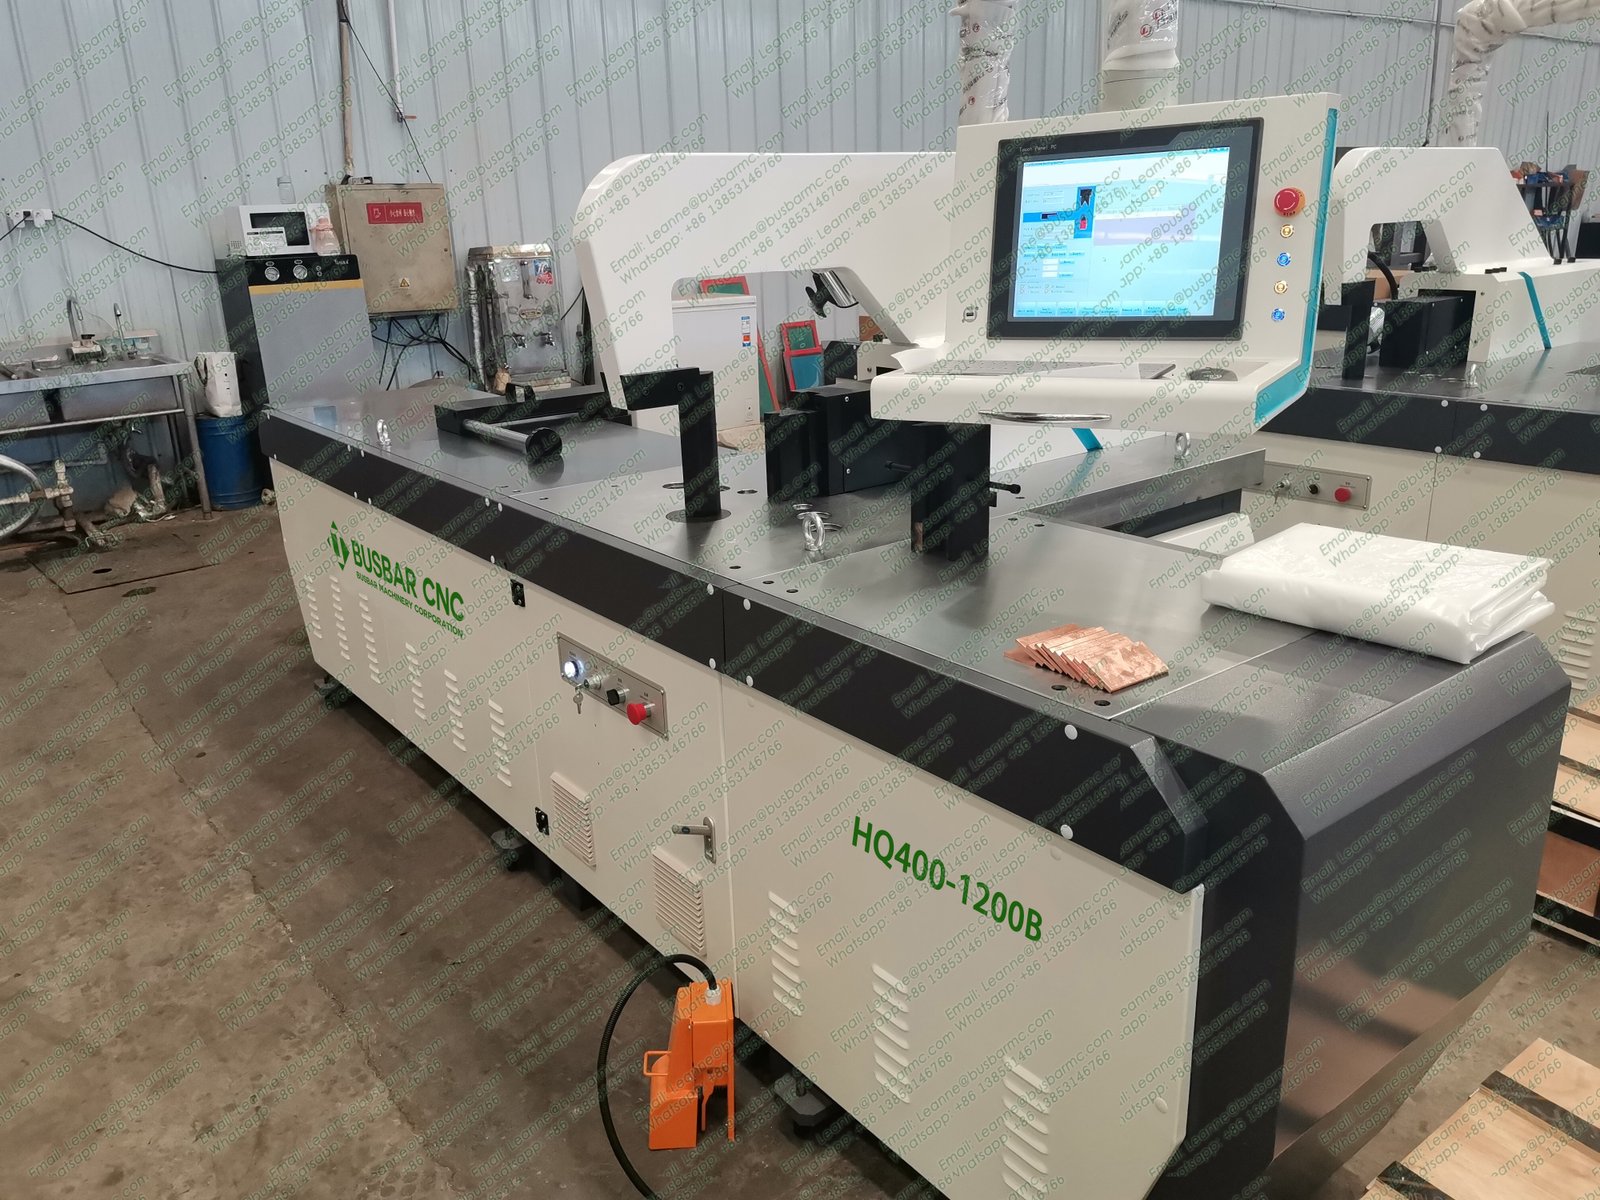
In production, “knowing how a bending machine works” is not enough. What matters is whether the same released angle and bend line stay stable across operators, shifts, and repeat orders. On a busbarmc bend station (303U-3-C / 503U-3-C / 803U-3-C), lock drawing revision → tooling → HMI mode/recipe → first-article measure → monitor first/mid/last parts. CNC/HMI reduces operator scatter; material and machine condition still dominate repeatability.
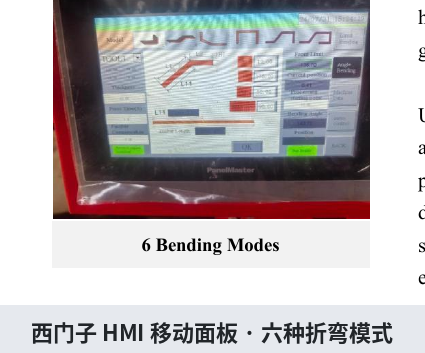
Siemens HMI mobile panel: bending modes screen
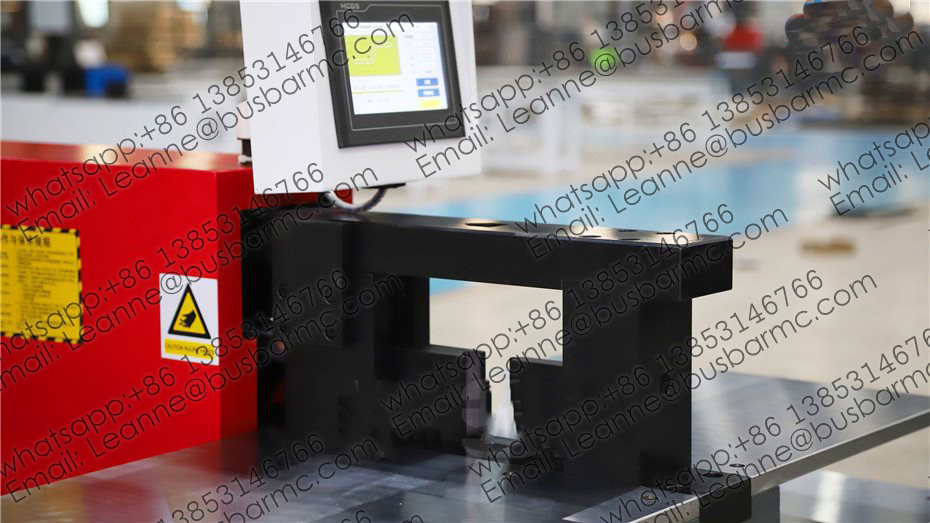
Bending unit with worktable and HMI (source: busbarmc.com)
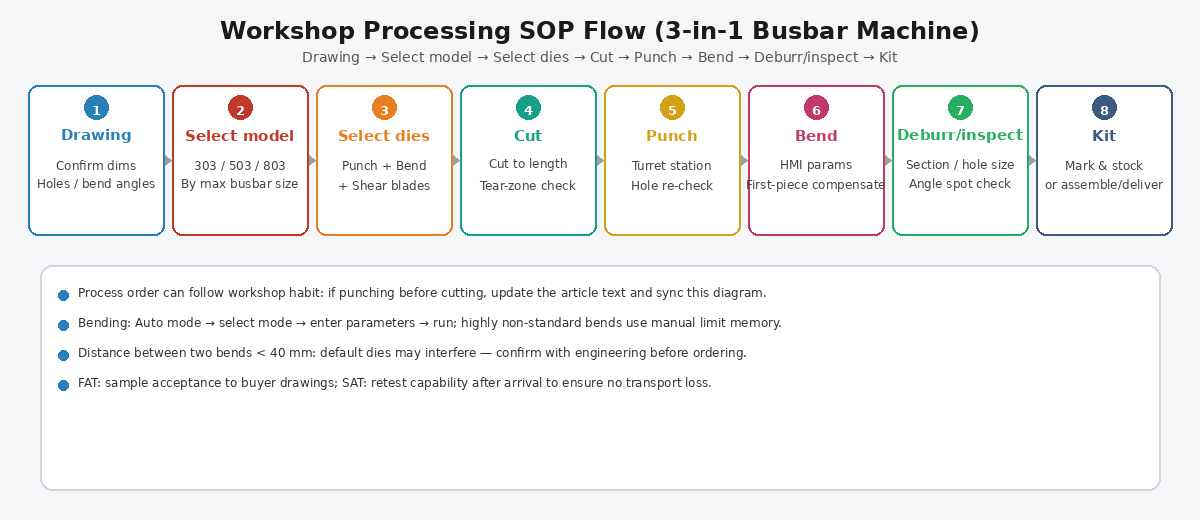
Workshop SOP flow: Drawing → Cut → Punch → Bend → Inspect
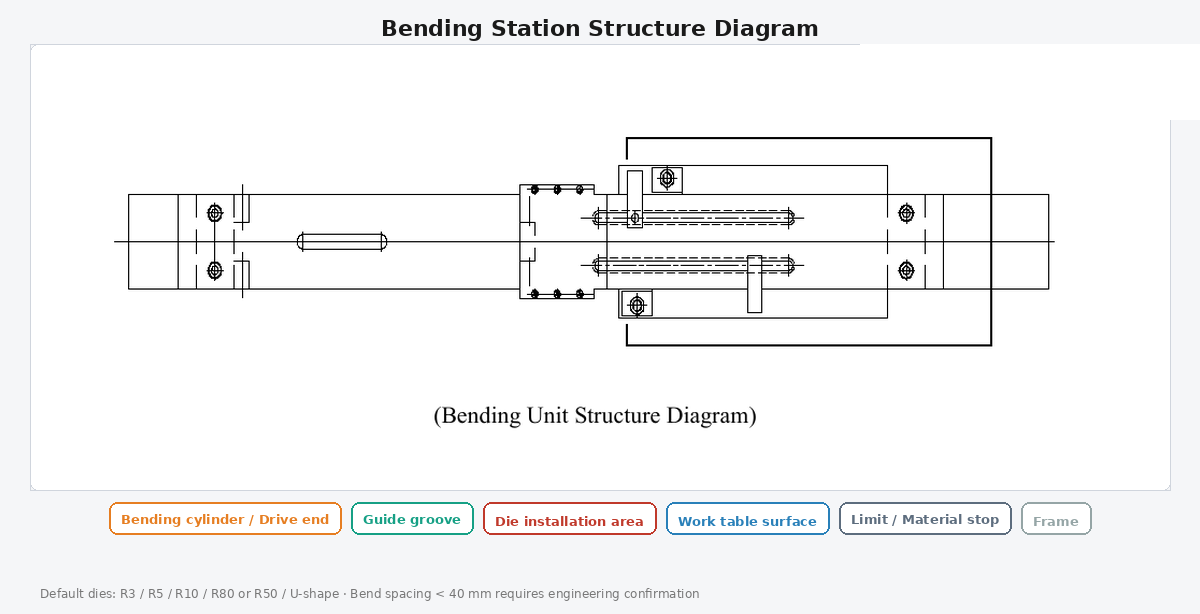
Bending station structure diagram (EN)
| Factor | Production symptom if ignored |
|---|---|
| Material lot / temper drift | Angle walks mid-batch |
| Hydraulic / oil temperature | Morning vs afternoon drift |
| Tool wear / radius change | Surface marks + angle shift |
| Recipe discipline between shifts | Operator A ≠ Operator B |
| Upstream cut/punch error | Bend cannot “fix” bad length/holes |
Bending alone never completes busbar fabrication—cut and punch errors still kill assembly fit.
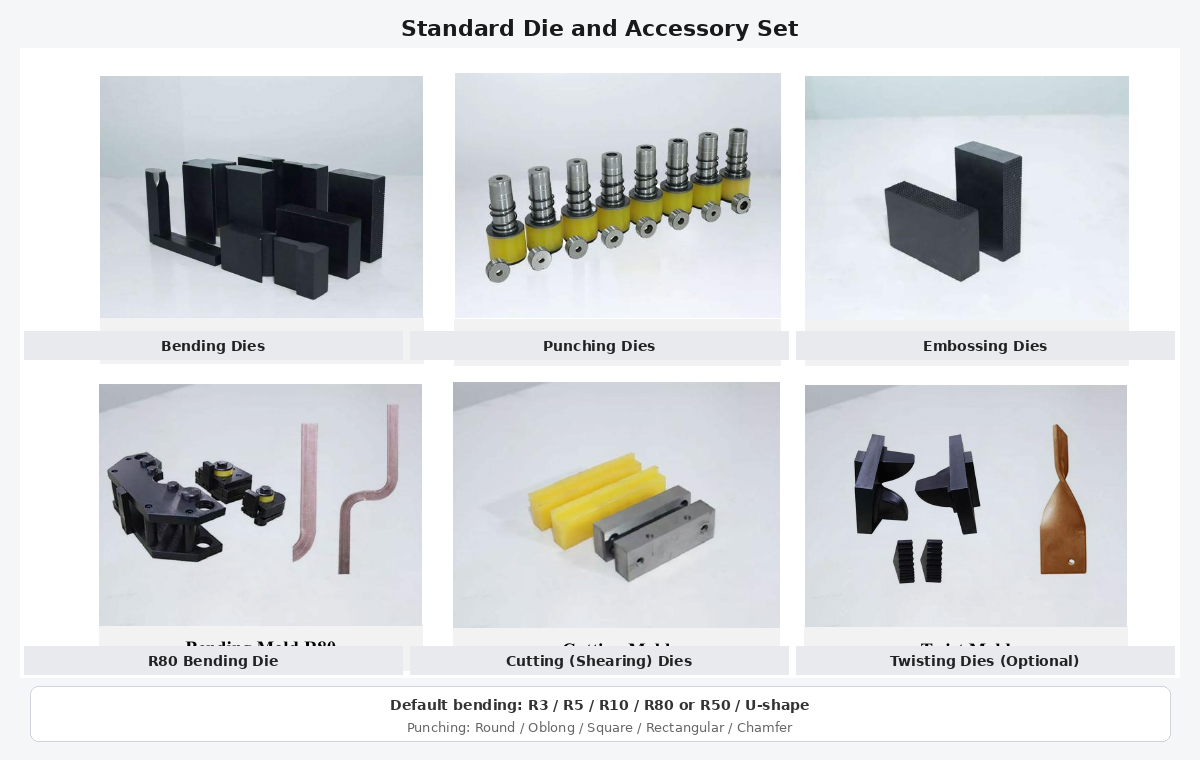
One bend station can cover many sizes only if dies and settings change with the drawing. HMI recipes make recall easier; die change and first-article remain mandatory.
Standard die and accessory set with English labels
There is no universal calendar. Replace or regrind when operators see accuracy drift or surface degradation. Track by condition and measured scrap, not guesswork.
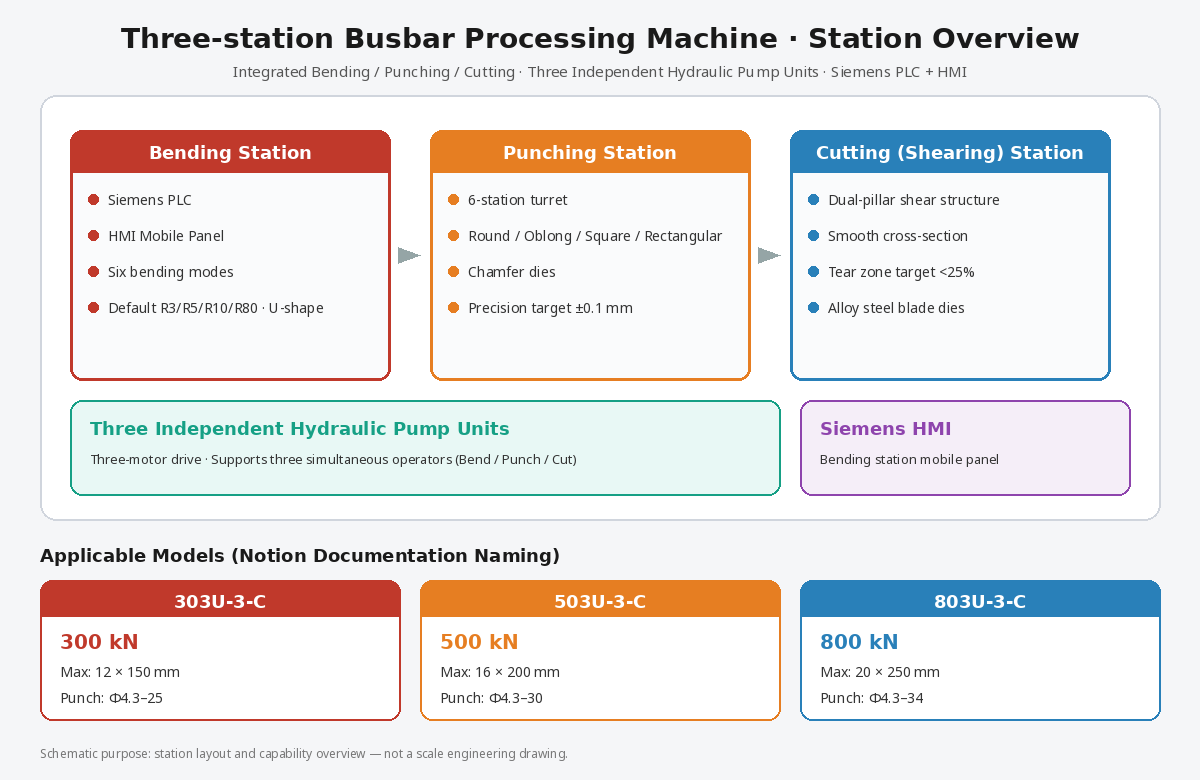
Three-station layout overview with English callouts
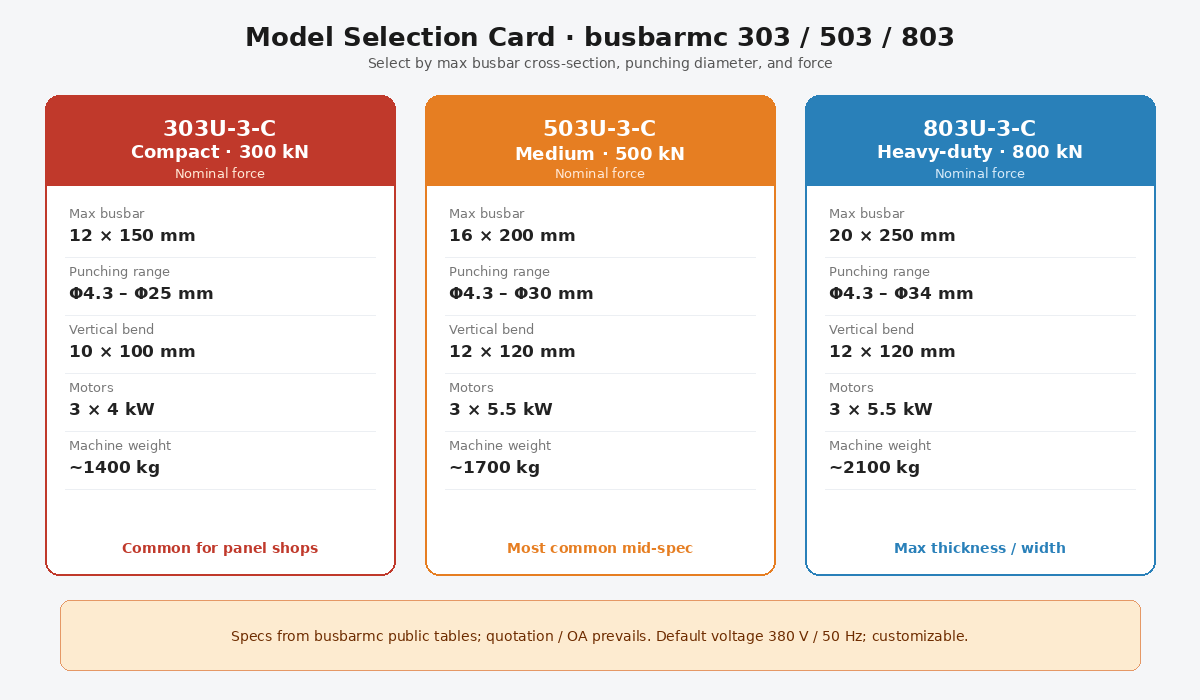
Model selection card: 303U-3-C / 503U-3-C / 803U-3-C
Use the bend station with punch/shear on one frame; three pump groups allow parallel staffing. Published flat/edge limits and ±1° / ±0.5° figures still need FAT proof on your copper/aluminum.
Yes, with die and setting changes. Recipes help; first-article still required.
By condition—when accuracy or surface worsens—not by a fixed month count alone.
Material stability, hydraulic condition, and whether shifts keep the same locked recipe.
No. Cutting, punching, and positioning all affect final assembly.
That page teaches principles & steps (incl. video-oriented structure). This page focuses on batch stability, changeover, and production metrics for GEO/buyers.